
3D Printer Nozzle MK8 0.6mm/1.75mm Brass (MT0486) Products
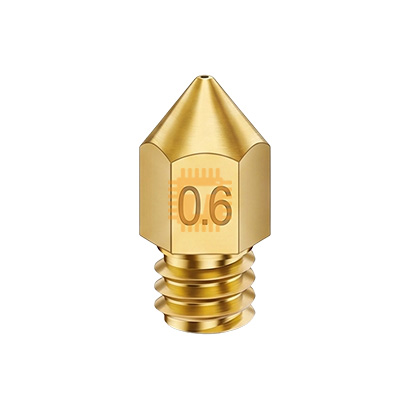
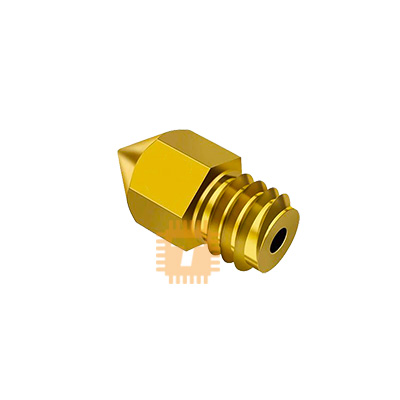
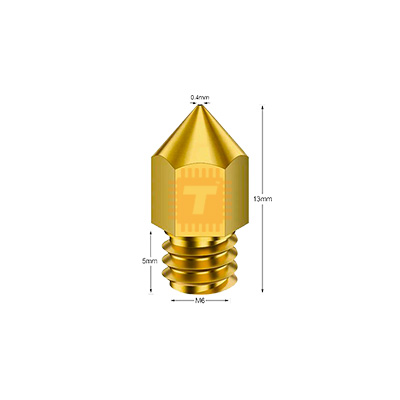
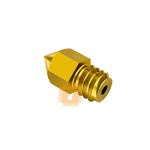
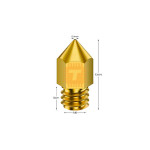
| Name | 3D Printer Nozzle MK8 0.6mm/1.75mm Brass |
| Code | MT0486 |
| Price | Rs.50.00 |
| In Stock | Yes |
| Package | CNC |
Product Details
The MK8 0.6mm Brass 3D Printer Nozzle is a high-efficiency, wide-bore extrusion nozzle engineered for MK8-style hotends across a broad range of desktop FDM 3D printers. Machined from high-purity, thermal-conductive brass with a precision 0.6mm orifice, this nozzle dramatically decreases print times while significantly increasing mechanical layer adhesion and structural part strength for standard 1.75mm filaments.
Specification
- Nozzle Standard: MK8 Profile
- Orifice Output Diameter: 0.6mm
- Filament Diameter Compatibility: 1.75mm
- Material Composition: High-Purity International Standard Brass (H59 / H62)
- Thermal Conductivity: Approx. 105 W/(m·K)
- Maximum Printing Temperature: Up to 260°C - 300°C
- Screw Thread Standard: Metric M6 (M6 x 1.0mm pitch)
- Total Length: 13mm
- Hex Flat Diameter: 6mm
- Inner Bore Roughness: Ra less than 0.4 µm
- Printer Compatibility: Compatible with standard MK8 hotend heater blocks, including Creality Ender-3 series, Ender-5 series, CR-10 series, Anet A8/A6, MakerBot Replicator, Tevo Tarantula, Anycubic Mega series, and other M6 MK8-threaded extruder assemblies.
Features
- Substantially Faster Print Times: The wider 0.6mm bore allows for wider line widths (0.6mm to 0.75mm) and taller layer heights (up to 0.45mm - 0.48mm), reducing print durations by up to 30% to 50% on large-scale models compared to standard 0.4mm nozzles.
- Superior Layer Bonding and Strength: Extruding wider beads of molten plastic maximizes contact surface area and thermal retention between layers, resulting in exceptionally strong and impact-resistant parts.
- High Thermal Transfer Brass Core: High-conductivity brass ensures rapid, uniform thermal transfer into the larger volume of filament passing through the melt chamber.
- Precision CNC Mirror-Bore: Polished internal geometry (Ra less than 0.4 µm) reduces internal friction and back-pressure, facilitating high volumetric flow rates and lowering the risk of clogs.
- Flat Contact Mating Face: The precision-machined rear shoulder provides a gap-free mechanical seal against the heatbreak throat or internal PTFE liner when properly hot-tightened.
Common Applications
- Large-Scale Functional Parts: Printing heavy-duty brackets, motor mounts, robotic chassis components, and utility fixtures where structural durability is prioritized over micro-detail.
- High-Speed Prototyping: Rapid fabrication of full-scale concept models, architectural volumes, and validation prototypes in a fraction of standard print times.
- Vase Mode (Spiralize Outer Contour): Producing thick, watertight single-wall containers, lamp shades, and decorative planters with substantial wall rigidity.
Professional Installation and Maintenance Tips
- Always Perform Final Hot-Tightening: Thread the nozzle into the heater block finger-tight while cold, heat the hotend to 240°C - 250°C, hold the heater block securely with an adjustable wrench, and torque the nozzle firmly with a 6mm socket (approx. 1.5 to 2.0 N·m) to prevent molten plastic leaks.
- Update Slicer Configuration: Change the nozzle diameter setting to 0.6mm in your slicer (Cura, PrusaSlicer, OrcaSlicer, Bambu Studio) and verify your volumetric flow limits and layer heights are scaled appropriately.
- Increase Hotend Temperature Slightly: Because a 0.6mm nozzle extrudes a greater volume of plastic per second, consider increasing the printing temperature by 5°C to 10°C to ensure complete filament melting at higher speeds.
- Avoid Abrasive and Filled Materials: Standard brass is soft and will quickly wear out if used with abrasive filaments containing carbon fiber, glass fiber, wood, or glow-in-the-dark additives. Use hardened steel or bi-metal nozzles for abrasive materials.
Sharing is caring, show love and share the product with your friends.
Featured

Add to Cart

Add to Cart

Other Products


Add to Cart
