
Solder Pot ZTX-31C 280W Adjustable Temperature Approx. 100-550C (TA1893) Products
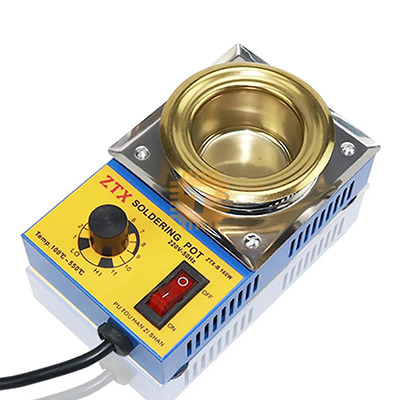
| Name | Solder Pot ZTX-31C 280W Adjustable Temperature Approx. 100-550C |
| Code | TA1893 |
| Price | Rs.3,400.00 |
| In Stock | Yes |
Product Details
The Solder Pot ZTX-31C 280W Adjustable Temperature Approx. 100-550C is a high-capacity, heavy-duty benchtop molten solder bath engineered for large-bundle wire harness tinning, heavy terminal dipping, motor coil and transformer de-enameling, and small-batch component rework. Powered by a high-output 280W ceramic heating core, it delivers rapid thermal recovery and consistent temperature stability to support high-throughput dipping cycles across an adjustable range of approximately 100°C to 550°C. Built with an expanded-diameter, corrosion-resistant titanium alloy / stainless steel crucible, it withstands both traditional leaded (Sn60/Pb40) and demanding lead-free (RoHS compliant) alloys without crucible erosion or bath contamination, making it a dependable solution for production lines, electrical rewinding shops, and electronics repair facilities.
Specifications
- Model: ZTX-31C
- Input Operating Voltage: 220V–240V AC, 50/60 Hz
- Rated Heating Power: 280 W
- Temperature Regulation Range: Approx. 100°C to 550°C (Adjustable via analog rotary dial)
- Crucible / Pot Diameter: Approx. 80 mm to 100 mm
- Crucible Depth: Approx. 40 mm to 45 mm
- Molten Solder Capacity: Approx. 800 g to 1500 g of solder alloy
- Melting Time / Warm-Up Rate: Approx. 8 to 15 minutes (From ambient to operational liquidus state)
- Crucible Material: High-Grade Titanium Alloy / Specially Treated Stainless Steel (Anti-corrosion, anti-acid, and erosion-resistant)
- Heating Element Type: High-Efficiency Mica-Insulated Ceramic Heating Assembly
- Temperature Control Method: Stepless Analog Potentiometer Dial with Power Indicator Lamp
- Chassis Construction: Heavy-Gauge Stamped Sheet Metal with High-Temperature Baked Enamel Finish
- Base Configuration: Low-Center-of-Gravity Stanchion Platform with Non-Slip Rubber Stabilizer Feet
- Mains Power Cord: Heavy-Duty 3-Core Grounded Power Cord
- Operating Ambient Temperature: 0°C to +40°C
- Net Weight: Approx. 900 g to 1250 g (Unloaded dry weight)
Features
- High-Power 280W Rapid Heating: Accelerates warm-up times and provides rapid thermal replenishment during continuous dipping of thick copper cables and large metal terminal lugs.
- Wide-Mouth Titanium Crucible: Large 80mm–100mm opening easily accommodates multi-pin connectors, wide cable looms, and bulky transformer windings without edge interference.
- Lead-Free & Leaded Solder Ready: Premium titanium alloy pot resists the leaching and pitting caused by high-tin, lead-free solder formulations, extending bath working life.
- Broad 100°C–550°C Thermal Envelope: Provides precise thermal settings for standard low-temperature leaded tinning up to intense enamel burn-off for magnet wires.
- Stable, Low-Profile Base: Wide, balanced footprint prevents tipping hazards on busy production benches, enhancing operator safety during high-volume operations.
Common Applications
- Heavy Gauge Wire & Cable Tinning: Dipping large stranded copper conductors, multi-conductor cable ends, and heavy automotive/battery ground leads.
- Transformer & Motor Stator Rework: Burning off high-temperature polyurethane or polyester enamel coatings on magnet wire while simultaneously tinning coil leads.
- Multi-Pin Connector & Terminal Dipping: Pre-tinning large connector blocks, spade terminals, ring lugs, and multi-pin automotive header pins.
- Batch Component Preparation: Pre-tinning axial/radial components, high-power resistors, and large inductors before circuit board assembly.
- Solder Dross Re-Melting & Recovery: Melting production solder scrap, bar ends, and wire cutoffs into reusable molten alloy or casting ingots.
Usage Tips
- Initial Burn-In & Crucible Seasoning (CRITICAL):
- Step 1: Pack the dry pot at least half full with solder bars or wire before powering the unit on. Never energize an empty solder pot, as heating a dry crucible causes rapid element burnout and surface oxidation.
- Step 2: Set the dial to ~300°C and allow the solder to melt down completely. Continue adding solder until the level sits roughly 5 mm to 8 mm below the top rim.
- Step 3: Use a non-contaminating metal rod or fluxed wire to wet the inside walls with liquid solder to establish an anti-oxidation barrier.
- Temperature Setting Recommendations:
- For standard 60/40 leaded alloys (melting point ~183°C–190°C), operate between 250°C and 280°C.
- For SAC305 / lead-free alloys (melting point ~217°C), operate between 280°C and 320°C.
- Use extreme temperatures (450°C–550°C) only when burning off stubborn enamel coatings on copper magnet wire. Avoid running continuously above 400°C during normal tinning, as excessive heat rapidly depletes flux and accelerates dross buildup.
- Dross Skimming Protocol: Due to the wide surface area of the ZTX-31C, an oxide film (dross) forms continuously on the surface of the bath. Skim the dross aside using a stainless steel scraper or wooden paddle immediately prior to each dip to ensure a bright, defect-free solder coat.
- Pre-Fluxing Routine: Dip bare copper leads or terminal lugs into a separate dish of liquid rosin flux before submerging them into the molten solder for 1 to 2 seconds. Pull leads out smoothly and steadily to form a uniform, reflective finish.
- Workplace Safety & Fume Control: Always connect to a verified, earthed mains socket. Because large molten baths emit significant heat and vaporized flux fumes, operate strictly beneath an active solder fume extractor or inside a ventilated production hood, and wear protective safety glasses and heat-resistant gloves.
Sharing is caring, show love and share the product with your friends.
Featured


Add to Cart

Add to Cart
Other Products


Add to Cart

Add to Cart
