
Solder Wire Lead Roll 63/37 0.8mm 50g High Quality (TA1894) Products
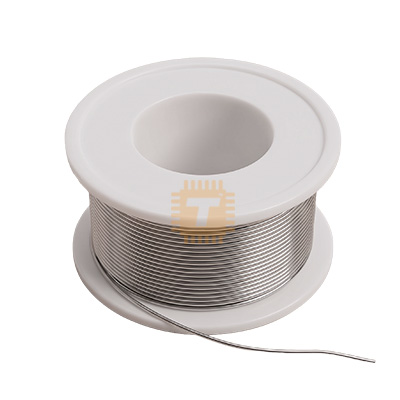
| Name | Solder Wire Lead Roll 63/37 0.8mm 50g High Quality |
| Code | TA1894 |
| Price | Rs.850.00 |
| In Stock | Yes |
| Package | SOLDER |
Product Details
The Solder Wire Lead Roll 63/37 0.8mm 50g High Quality is a true eutectic tin-lead alloy soldering wire engineered for high-reliability through-hole PCB assembly, electronic component repair, cable harness termination, and general-purpose rework. Formulated with a precise metallurgical ratio of 63% Tin (Sn) and 37% Lead (Pb), it features a sharp, singular eutectic melting point at exactly 183°C (361°F), completely eliminating the semi-solid "pasty range" during cooling. Equipped with a continuous, high-grade rosin flux core centered along its versatile 0.8mm wire gauge, it provides instantaneous wetting, rapid capillary draw, and mirror-bright, concave solder fillets without disturbing delicate joints during solidification.
Specifications
- Alloy Composition: 63% Tin (Sn) / 37% Lead (Pb) (Eutectic Alloy)
- Wire Diameter Gauge: 0.8 mm (Approx. 0.031 Inches / Ideal balance for SMD and THT)
- Net Alloy Weight: 50 g (Excluding spool tare weight)
- Quality Standard: High Quality (High-purity virgin alloy with uniform flux core distribution)
- Melting Characteristics:
- Eutectic Melting Point: Exactly 183°C (361°F)
- Solidus Temperature: 183°C
- Liquidus Temperature: 183°C
- Pasty Range: 0°C (Transitions instantly from liquid to solid without intermediate plastic phase)
- Flux Core Type: High-Grade Activated Rosin Core (RA / RMA Type, Non-Corrosive)
- Flux Content / Percentage: 1.8% to 2.2% Core by Weight
- Flux Halide Content: < 0>
- Solder Joint Appearance: Mirror-Bright, Shiny, and Smooth Concave Fillet
- Residue Characteristics: Amber/Clear, Non-Conductive, and Non-Corrosive Rosin Residue
- Spool Construction: High-Impact Rigid Thermoplastic Reel with Smooth De-Reeling Arbor
- Spool Dimensions: Approx. 45 mm Flange Diameter × 28 mm Height (Arbor hole: ~15 mm)
- Gross Weight: Approx. 65 g to 75 g (Wire and spool combined)
Features
- True Eutectic Freezing (Zero Pasty Range): Solidifies instantly upon cooling past 183°C, drastically reducing the risk of "cold" or "disturbed" solder joints caused by accidental component vibration during cooling.
- Versatile 0.8mm All-Rounder Diameter: Delivers the optimal solder volume per millimeter for standard through-hole DIP ICs, passive resistors/capacitors, pin headers, and medium SMD pads (1206/0805).
- Instant Wetting & Superior Capillary Flow: High-purity tin-lead alloy combined with an active multi-channel rosin core breaks through surface oxide layers on copper, brass, and tin plate in under a second.
- Non-Corrosive High-Impedance Residue: Dries into an inert, non-conductive rosin barrier with high surface insulation resistance (SIR), safe to leave on standard commercial boards without fear of trace degradation.
- Low Spatter & Minimal Fuming: Carefully formulated flux core minimizes popping, solder spatter, and micro-balling during rapid thermal contact, keeping the surrounding PCB layout clean.
Common Applications
- Through-Hole PCB Assembly: Hand-soldering DIP integrated circuits, pin headers, terminal blocks, radial/axial capacitors, and discrete passive components.
- Cable & Wire Harness Assembly: Tinning stranded copper conductors, soldering automotive/marine wiring harnesses, and securing DC barrel jacks.
- Audio & Musical Equipment Repair: Soldering audio potentiometers, guitar pickups, 1/4-inch phono jacks, XLR connectors, and vintage amplifier circuits.
- Robotics & Drone Prototyping: Securing battery leads (XT60, Deans), electronic speed controller (ESC) power pads, and brushless motor leads.
- Educational Prototyping: Ideal for students, hobbyists, and makers assembling circuits on perfboards, stripboards, and copper clad protoboards.
Usage Tips
- Iron Temperature Setting:
- Due to the low eutectic melting point of 183°C, set your soldering iron tip between 300°C and 340°C (572°F to 644°F).
- Avoid running the iron above 360°C; excessive heat rapidly burns away the rosin flux before it can deoxidize the joint, leaving oxidized, frosty surfaces.
- Proper Soldering Sequence:
- Touch the tinned iron tip simultaneously to the component lead and the PCB copper pad to heat both parts for 1 to 2 seconds.
- Feed the 0.8mm solder wire directly into the heated joint—not directly onto the iron tip. Once the solder flows smoothly around the lead to form a shiny concave fillet, withdraw the wire first, then cleanly lift the iron tip away.
- Residue Cleaning (Optional): While the rosin flux residue is non-conductive and chemically non-corrosive under normal operating conditions, clean sensitive RF, high-impedance analog, or high-voltage circuits using an ESD-safe brush and Isopropyl Alcohol (IPA ≥ 99%).
- Health & Environmental Safety:
- Contains elemental lead (Pb). Always wash hands thoroughly with soap and water after handling solder wire, and never eat or drink near the soldering workbench.
- Work in a well-ventilated space or use an active benchtop solder fume extractor to pull rosin flux smoke and airborne particulate away from your breathing zone.
- Storage Recommendations: Store the spool in a dry, low-humidity environment away from direct sunlight or corrosive chemicals to prevent surface tarnishing and maintain rapid wetting performance over years of use.
Sharing is caring, show love and share the product with your friends.
Featured


Add to Cart
Add to Cart
Other Products

Add to Cart


