
3D Printer Nozzle MK8 0.2mm/1.75mm Brass (MT0482) Products
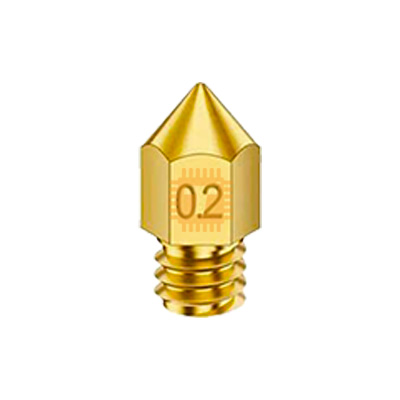
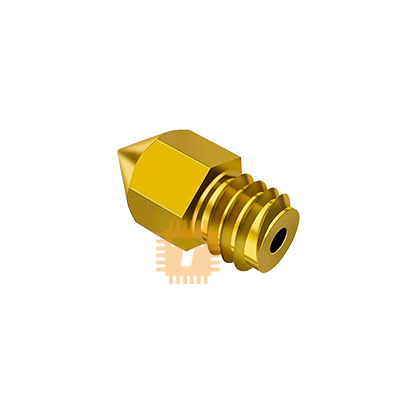
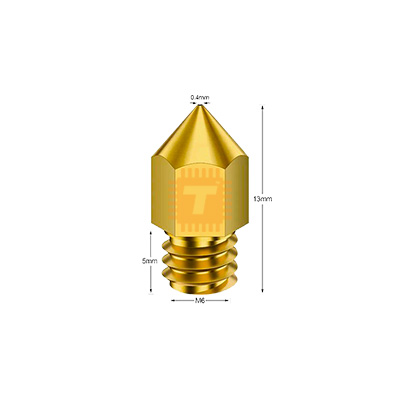
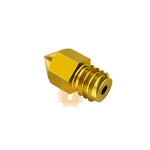
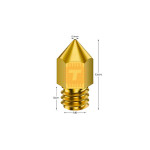
| Name | 3D Printer Nozzle MK8 0.2mm/1.75mm Brass |
| Code | MT0482 |
| Price | Rs.50.00 |
| In Stock | Yes |
| Package | CNC |
Product Details
The MK8 0.2mm Brass 3D Printer Nozzle is an ultra-fine extrusion nozzle engineered for MK8-style hotends across a wide range of desktop FDM 3D printers. Crafted from high-purity, thermal-conductive brass with a precision CNC-machined micro-orifice, this nozzle allows for exceptionally thin layer heights, sharp corners, and intricate detailing on 1.75mm filament prints, making it an essential upgrade for high-resolution micro-prototyping and miniature fabrication.
Specification
- Nozzle Standard: MK8 Profile
- Orifice Output Diameter: 0.2mm
- Filament Diameter Compatibility: 1.75mm
- Material Composition: High-Conductivity International Standard Brass (H59 / H62)
- Thermal Conductivity: Approx. 105 W/(m·K)
- Maximum Printing Temperature: Up to 260°C - 300°C
- Screw Thread Standard: Metric M6 (M6 x 1.0mm pitch)
- Total Length: 13mm
- Hex Flat Diameter: 6mm
- Inner Bore Roughness: Ra less than 0.4 µm
- Printer Compatibility: Compatible with standard MK8 extruder heater blocks, including Creality Ender-3 series, Ender-5 series, CR-10 series, Anet A8, MakerBot, and other M6 MK8-compatible hotends.
Features
- Ultra-Fine Micro-Orifice: The 0.2mm aperture diameter enables ultra-thin layer deposition (down to 0.08mm - 0.12mm) for smooth vertical walls and razor-sharp horizontal details that standard 0.4mm nozzles cannot achieve.
- High Thermal Transfer Brass Core: High-grade brass ensures rapid, uniform thermal conductivity across the melt zone, allowing consistent filament flow even at tiny extrusion volumes.
- Precision CNC Chamfer and Internal Mirror Polish: Features a smooth internal taper and polished bore (Ra less than 0.4 µm) to reduce wall friction and prevent micro-cavitation and clogging during low-flow extrusion.
- Flat Contact Mating Face: The precision-ground flat rear interface ensures a gap-free mechanical seal against the internal heatbreak throat or PTFE tube when hot-tightened, preventing filament leakage along the heater block threads.
Common Applications
- Miniatures and Figurine Printing: Fabricating tabletop gaming figurines, scale models, and detailed statues where fine facial features, weapons, and textures are essential.
- Precision Text and Jewelry Molds: Printing micro-text, detailed jewelry master casts, embossed badges, and fine logos requiring sharp surface edges.
- Fine Mechanical and Dental Prototyping: Producing small gears, watch components, tight-tolerance electronic enclosures, and detailed orthodontic study models.
Professional Installation and Maintenance Tips
- Always Perform Final Hot-Tightening: Thread the nozzle into the heater block finger-tight while cold, heat the hotend to roughly 240°C - 250°C, hold the heater block securely with a wrench, and give the nozzle a gentle final torque with a 6mm socket (approx. 1.5 to 2.0 N·m) to prevent leaks.
- Adjust Slicer Settings for Low Flow: Reduce print speeds (typically 20mm/s to 35mm/s) and adjust retraction distance and speed down to prevent back-pressure jams, as a 0.2mm hole creates significantly higher extrusion back-pressure than a standard 0.4mm nozzle.
- Use Clean, High-Quality Filaments: Ultra-fine 0.2mm nozzles are sensitive to dust and foreign particles. Always use clean, dry filament and consider adding a foam filament dust filter on the spool feed line to avoid clogs.
- Avoid Abrasive and Filled Materials: Never use composite filaments containing carbon fiber, wood, glow-in-the-dark particles, or metal powders with a 0.2mm brass nozzle, as particles will cause immediate physical blockages and rapidly erode soft brass.
Sharing is caring, show love and share the product with your friends.
Featured

Add to Cart


Other Products

Add to Cart

Add to Cart
Add to Cart

