
3D Printer Nozzle MK8 0.8mm/1.75mm Brass (MT0487) Products
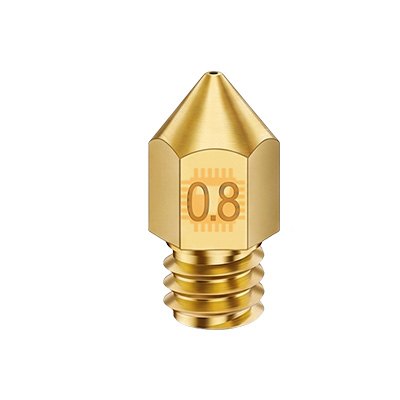
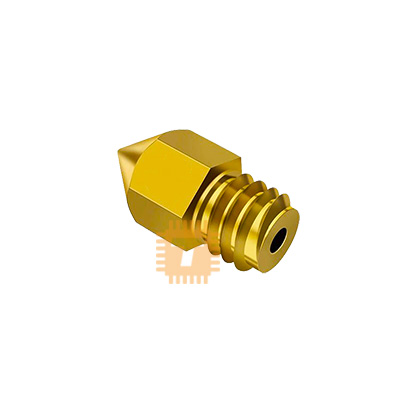
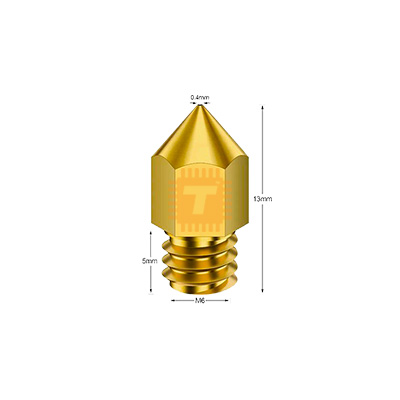
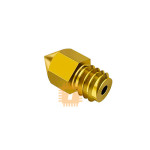
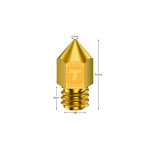
| Name | 3D Printer Nozzle MK8 0.8mm/1.75mm Brass |
| Code | MT0487 |
| Price | Rs.50.00 |
| In Stock | Yes |
| Package | CNC |
Product Details
The MK8 0.8mm Brass 3D Printer Nozzle is an ultra-high-flow extrusion nozzle designed for MK8-style hotends across a wide range of desktop FDM 3D printers. Machined from high-purity, thermally conductive brass with an enlarged 0.8mm orifice, this nozzle is engineered to output massive volumetric flow rates, drastically slashing print times on large-scale models while producing thick, incredibly durable layer bonds for standard 1.75mm filaments.
Specification
- Nozzle Standard: MK8 Profile
- Orifice Output Diameter: 0.8mm
- Filament Diameter Compatibility: 1.75mm
- Material Composition: High-Purity International Standard Brass (H59 / H62)
- Thermal Conductivity: Approx. 105 W/(m·K)
- Maximum Printing Temperature: Up to 260°C - 300°C
- Screw Thread Standard: Metric M6 (M6 x 1.0mm pitch)
- Total Length: 13mm
- Hex Flat Diameter: 6mm
- Inner Bore Roughness: Ra less than 0.4 µm
- Printer Compatibility: Compatible with standard MK8 hotend heater blocks, including Creality Ender-3 series, Ender-5 series, CR-10 series, Anet A8/A6, MakerBot Replicator, Tevo Tarantula, Anycubic Mega series, and other M6 MK8-threaded extruder assemblies.
Features
- Massive Time Savings on Large Prints: The wide 0.8mm aperture enables line widths from 0.8mm to 1.0mm and layer heights up to 0.6mm, cutting total print times by 50% to 70% on large-format components compared to standard 0.4mm nozzles.
- Maximum Mechanical Part Strength: Thick extruded beads provide exceptional layer contact surface area and thermal retention, resulting in parts with immense impact resistance and near-isotropic layer bonding.
- High Thermal Transfer Brass Core: High-conductivity brass transfers heat rapidly into the fast-moving, high-volume filament core to prevent cold under-extrusion.
- Smooth CNC Mirror-Bore: The polished internal cavity (Ra less than 0.4 µm) minimizes wall friction and back-pressure, ensuring consistent flow under heavy extrusion demands.
- Flat Contact Sealing Face: Precision-machined rear shoulder provides a gap-free mechanical seal against the heatbreak throat or internal PTFE liner when properly hot-tightened, preventing leakage along the heater block threads.
Common Applications
- Heavy-Duty Functional & Industrial Parts: Printing load-bearing brackets, structural frames, workshop jigs, battery enclosures, and robotic base plates where rugged strength is paramount.
- Large-Scale Prototyping & Cosplay: Rapid fabrication of full-scale architectural models, cosplay armor, helmets, and large concept sculptures with minimum build times.
- Single-Wall Spiralize / Vase Mode: Producing rigid, completely watertight planters, waste bins, lampshades, and containers with thick, structural single walls.
Professional Installation and Maintenance Tips
- Always Perform Final Hot-Tightening: Thread the nozzle into the heater block finger-tight while cold, heat the hotend to 240°C - 250°C, hold the heater block securely with a wrench or pliers, and torque the nozzle firmly with a 6mm socket (approx. 1.5 to 2.0 N·m) to prevent plastic leakage past the threads.
- Increase Hotend Temperature by 10°C - 15°C: Because an 0.8mm nozzle pushes a significantly higher volume of plastic per second, raising your print temperature ensures complete filament melting and prevents extruder motor skipping.
- Calibrate Slicer Flow Limits: Update your slicer nozzle diameter to 0.8mm, set line width to 0.8mm - 0.95mm, and verify that your print speeds do not exceed your hotend's maximum volumetric flow rate (typically 12 - 15 mm³/s on standard MK8 hotends).
- Avoid Abrasive Composite Filaments: Soft brass will rapidly degrade when used with abrasive materials like carbon fiber, glass fiber, wood, or glow-in-the-dark filaments. Use hardened steel or bi-metal nozzles for abrasive composites.
Sharing is caring, show love and share the product with your friends.
Featured

Add to Cart


Other Products

Add to Cart


Add to Cart

Add to Cart
