
Solder Wire Lead Roll 63/37 0.8mm 100g High Quality (TA1895) Products
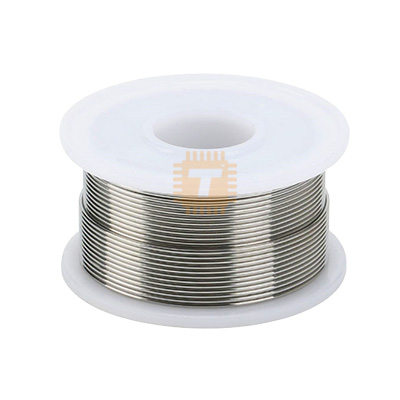
| Name | Solder Wire Lead Roll 63/37 0.8mm 100g High Quality |
| Code | TA1895 |
| Price | Rs.1,600.00 |
| In Stock | Yes |
| Package | SOLDER |
Product Details
The Solder Wire Lead Roll 63/37 0.8mm 100g High Quality is an extended-capacity spool of true eutectic tin-lead alloy soldering wire engineered for production-line electronics assembly, professional PCB rework, wire harness fabrication, and continuous benchtop repair. Formulated with an exact metallurgical ratio of 63% Tin (Sn) and 37% Lead (Pb), it features a sharp, singular eutectic melting transition at exactly 183°C (361°F), completely bypassing the semi-solid "pasty range" during solidification. Centered along its versatile 0.8mm diameter is a continuous, high-grade activated rosin flux core that delivers instantaneous wetting, rapid capillary spread, and mirror-bright, concave solder joints with high mechanical and electrical reliability.
Specifications
- Alloy Composition: 63% Tin (Sn) / 37% Lead (Pb) (True Eutectic Formulation)
- Wire Diameter Gauge: 0.8 mm (Approx. 0.031 Inches / Ideal balance for SMD and THT)
- Net Alloy Weight: 100 g (Excluding spool tare weight)
- Quality Standard: High Quality (High-purity virgin alloy with consistent flux core continuity)
- Melting Characteristics:
- Eutectic Melting Point: Exactly 183°C (361°F)
- Solidus Temperature: 183°C
- Liquidus Temperature: 183°C
- Pasty Range: 0°C (Transitions instantly from liquid to solid without intermediate plastic phase)
- Flux Core Type: High-Grade Activated Rosin Core (RA / RMA Type, Non-Corrosive)
- Flux Content / Percentage: 1.8% to 2.2% Core by Weight
- Flux Halide Content: < 0>
- Solder Joint Appearance: Mirror-Bright, Shiny, and Smooth Concave Fillet
- Residue Characteristics: Amber/Clear, Non-Conductive, and Non-Corrosive Rosin Residue
- Spool Construction: High-Impact Rigid Thermoplastic Reel with Smooth De-Reeling Arbor
- Spool Dimensions: Approx. 54 mm Flange Diameter × 28 mm Height (Arbor hole: ~19 mm to 20 mm)
- Gross Weight: Approx. 115 g to 130 g (Wire and spool combined)
Features
- True Eutectic Solidification: Freezes instantly upon cooling past 183°C, eliminating disturbed or crystalline cold joints caused by slight component movement during cooling.
- Extended 100g Production Spool: Provides double the wire capacity of standard 50g hobby spools, minimizing reel changes on busy technician benches and assembly stations.
- Versatile 0.8mm Wire Gauge: Delivers the optimal solder volume per millimeter for through-hole DIP ICs, passive components, terminal blocks, pin headers, and medium SMD footprints (1206/0805).
- Instant Wetting & Capillary Flow: High-purity tin-lead alloy combined with an active rosin core strips surface oxidation from copper pads, brass pins, and tinned leads in under a second.
- Non-Corrosive High-Impedance Residue: Dries into an inert, non-conductive rosin shield with high surface insulation resistance (SIR), safe to leave on standard commercial boards without fear of trace degradation.
- Low Spatter & Minimal Fuming: Carefully formulated flux core minimizes popping, solder spatter, and micro-balling during rapid thermal contact, keeping the surrounding PCB clean.
Common Applications
- Through-Hole PCB Assembly: Hand-soldering DIP integrated circuits, pin headers, terminal blocks, radial/axial capacitors, and discrete passive components.
- High-Volume Bench Repair & Rework: Daily maintenance and component replacement in electronics repair shops, audio gear service centers, and R&D laboratories.
- Cable & Wire Harness Assembly: Tinning stranded copper conductors, soldering automotive/marine wiring harnesses, and securing DC barrel jacks.
- Robotics & Drone Prototyping: Securing battery leads (XT60, Deans), electronic speed controller (ESC) power pads, and brushless motor leads.
- Educational STEM & Maker Prototyping: Circuit fabrication on copper-clad protoboards, stripboards, and point-to-point wiring projects.
Usage Tips
- Iron Temperature Calibration:
- Due to the low eutectic melting point of 183°C, set your soldering iron tip between 300°C and 340°C (572°F to 644°F).
- Avoid running the iron above 360°C; excessive heat rapidly burns away the rosin flux before it can deoxidize the joint, leaving oxidized, frosty surfaces.
- Proper Soldering Sequence:
- Touch the tinned iron tip simultaneously to the component lead and the PCB copper pad to heat both parts for 1 to 2 seconds.
- Feed the 0.8mm solder wire directly into the heated joint—not directly onto the iron tip. Once the solder flows smoothly around the lead to form a shiny concave fillet, withdraw the wire first, then cleanly lift the iron tip away.
- Residue Cleaning (Optional): While the rosin flux residue is non-conductive and chemically non-corrosive under normal operating conditions, clean sensitive RF, high-impedance analog, or high-voltage circuits using an ESD-safe brush and Isopropyl Alcohol (IPA ≥ 99%).
- Health & Environmental Safety:
- Contains elemental lead (Pb). Always wash hands thoroughly with soap and water after handling solder wire, and never eat or drink near the soldering workbench.
- Work in a well-ventilated space or use an active benchtop solder fume extractor to pull rosin flux smoke and airborne particulate away from your breathing zone.
- Spool Holder Mounting: The center arbor hole fits standard desktop soldering iron stand reel spindles, allowing smooth, snag-free wire feeding with one hand during assembly.
Sharing is caring, show love and share the product with your friends.
Featured

Add to Cart


Add to Cart


