TWO TREES Blue Nano Coated Engraving Bit (0.8-3.175mm) 10pcs (TA1874) Products

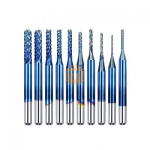
| Name | TWO TREES Blue Nano Coated Engraving Bit (0.8-3.175mm) 10pcs |
| Code | TA1874 |
| Price | Rs.6,800.00 |
| In Stock | Yes |
| Package | ACC |
Product Details
The TWO TREES Blue Nano-Coated Engraving Bit Set (0.8–3.175mm, 10 Pcs) is a professional assortment of micro-grain solid tungsten carbide end mills engineered for precision CNC routing, PCB isolation milling, 3D relief carving, and profile contouring. Enhanced with a high-durability Blue Nano composite coating, these corn-tooth/fish-tail style router bits deliver superior surface hardness, reduced cutting friction, and extended tool life across a wide variety of materials, including FR-4 circuit boards, hardwoods, acrylic, carbon fiber, and aluminum composites.
Specification
- Brand / Manufacturer: TWO TREES
- Product Name: Blue Nano Coated CNC Milling / Engraving Bit Set
- Quantity: 10 Pieces per Set (Assorted Sizes with Individual Protective Storage Case)
- Cutting Diameters Included: 0.8mm, 1.0mm, 1.2mm, 1.4mm, 1.6mm, 1.8mm, 2.0mm, 2.2mm, 2.5mm, and 3.175mm (1/8")
- Shank Diameter: 3.175mm (1/8" Standard CNC Collet Size)
- Overall Length (OAL): Approx. 38mm
- Cutting Edge Length (Flute Length): Approx. 5.5mm to 12mm (scaled proportionally by diameter)
- Substrate Material: Ultra-Fine Micro-Grain Solid Tungsten Carbide (Cemented Carbide)
- Surface Coating: Blue Nano (AlTiN / Nano-Composite Coating)
- Coating Hardness: Up to HV 3000 – 3500 (Heat resistance up to 800°C)
- Cutting Geometry: Corn-Tooth / Diamond-Pattern Rasp Flutes with Fish-Tail Plunge End
- Spindle Compatibility: Fits standard 1/8" (3.175mm) ER11, ER16, ER20 collets, trim router adapters, and rotary tool chucks.
Features
- Blue Nano Composite Coating: Provides a high-hardness, low-friction protective barrier that withstands high cutting temperatures (up to 800°C), preventing chip welding and dramatically increasing cutting life over uncoated carbide.
- Micro-Grain Tungsten Carbide Core: High-density carbide construction provides exceptional rigidity and edge retention, minimizing tool deflection and chatter during high-speed CNC milling.
- Corn-Tooth / Fish-Tail Cutting Geometry: Diamond-knurled cutting edges actively shear fibers and shred chips into fine dust, preventing edge burring, layer delamination, and top-surface tear-out on composite sheets and laminate boards.
- Universal 1/8" (3.175mm) Shank: Standardized shank diameter ensures drop-in compatibility with CNC 3018 PRO, Genmitsu, Two Trees TTC450/TTC300S, Shapeoko, and handheld rotary tools without requiring collet swaps.
- Versatile Incremental Sizing: Ten distinct cutter diameters from 0.8mm up to 3.175mm provide the ideal tool for intricate PCB trace isolation, tight-corner pocketing, deep contour slots, and perimeter roughing.
Common Applications
- PCB Isolation Milling & Drilling: Rapid prototyping of custom double/single-sided FR-4 and copper-clad circuit boards with clean, burr-free trace separation.
- Hardwood & Plywood 2D/3D Carving: Intricate relief sculpting, signage lettering, fretwork, and detailed craft routing in oak, walnut, bamboo, and MDF.
- Acrylic & Engineering Plastics: Precision cutting and slotting in Cast Acrylic (PMMA), Polycarbonate, Delrin/POM, Nylon, and ABS without melt buildup.
- Composite Sheet Routing: Clean edge cutting and hole drilling in Carbon Fiber plates, fiberglass (G10/FR4), and Aluminum Composite Panels (ACP/Dibond).
Professional Operation and Maintenance Tips
- Match Feed Rates to Bit Diameter: Smaller diameter bits (0.8mm to 1.4mm) have delicate stems; reduce plunge and feed rates (recommended plunge: 100–300 mm/min, feed: 300–800 mm/min) with light depth-per-pass (0.2mm–0.5mm) to avoid snapping the tool.
- Maximize Spindle Speed for Clean Cuts: Carbide micro-tools perform best at high surface speeds. Run spindles between 12,000 RPM and 24,000 RPM for smooth finishes and minimal cutting resistance.
- Use Proper Collet Seating: Insert at least 20mm of the shank into the ER collet to maximize clamping surface area and minimize tool runout; never clamp directly on the cutting flutes or the transition taper.
- Implement Active Dust Collection or Air Assist: The corn-tooth profile produces fine powdered chips. Using an air blast or active vacuum shoe prevents chips from re-packing inside deep cut channels, reducing friction and extending tool life.
Sharing is caring, show love and share the product with your friends.
Featured

Add to Cart


Add to Cart
Add to Cart